Guangdong Yipomson Electric Co., Ltd.
Email: caroline@yipomson.com
Hot Categories
Detail
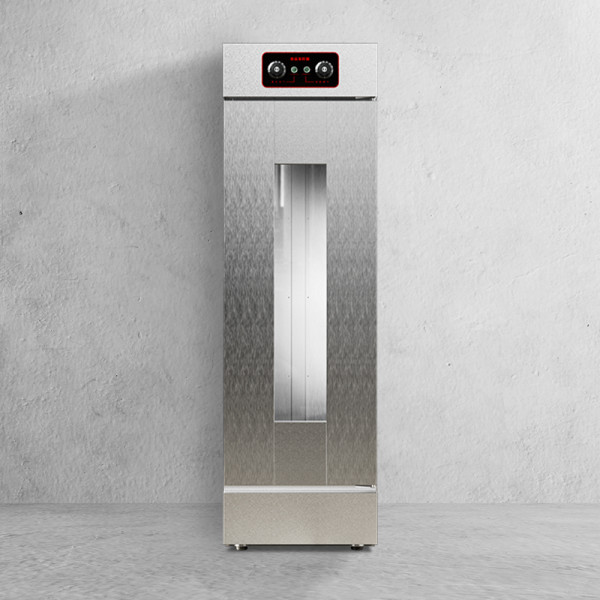
- Product NameFermenting box proofer bread ferment box
- Item NO.BG-66541971
- Weight0.0000 kg = 0.0000 lb = 0.0000 oz
- CategoryBakery Equipment> Proofer
- TagBossgoo, B2B, Bakery Equipment, Proofer
- Creation Time2026-10-12
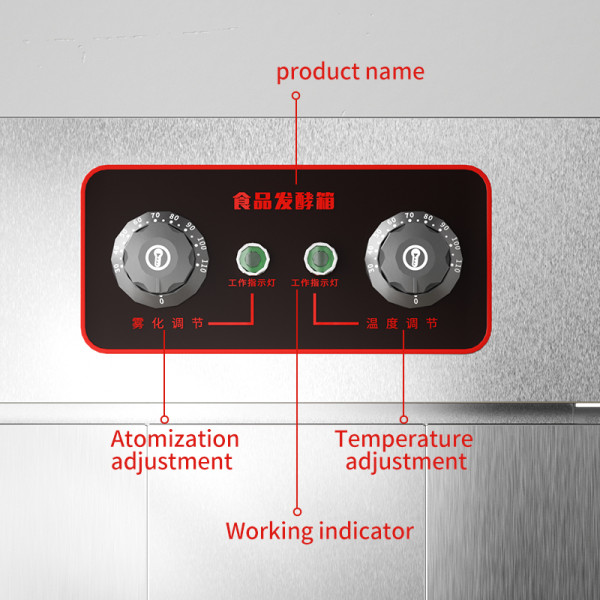
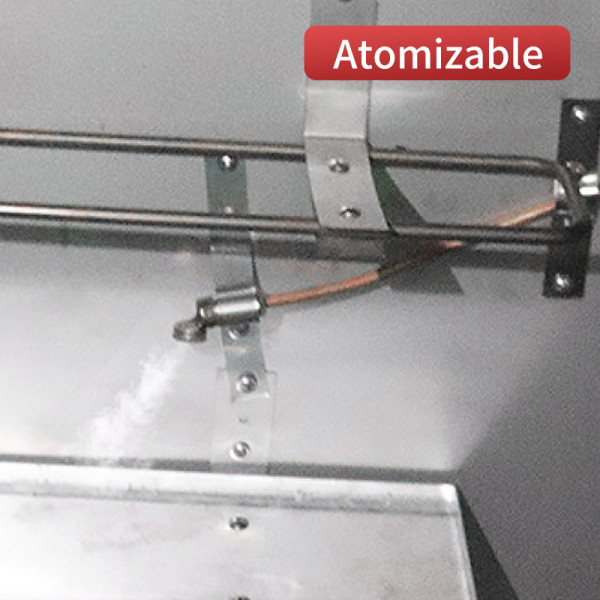
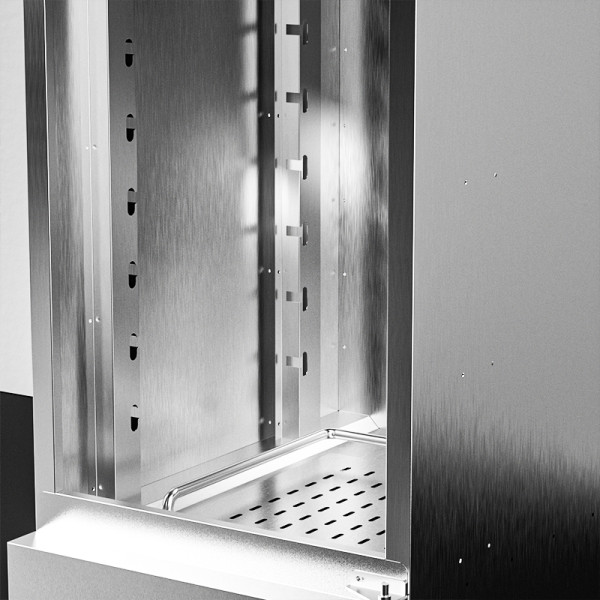
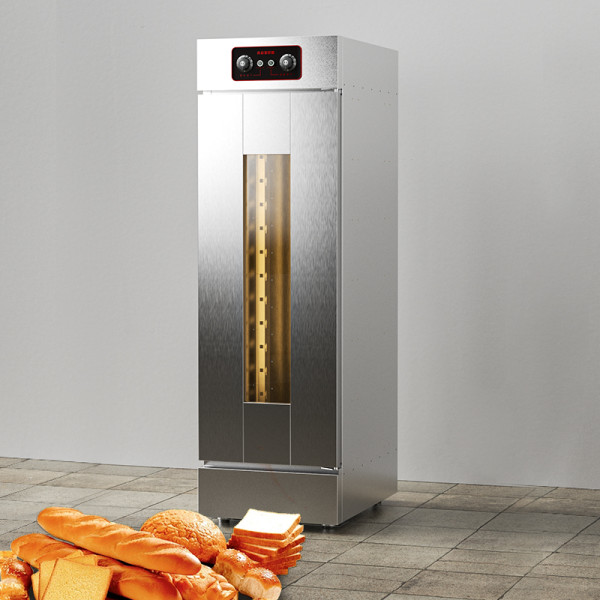
- High quality factory price industrial high-tech bread baking machine price fermentation tank Product overview Commercial food fermentation equipment is specially designed for the food industry, used to promote the growth and metabolism of microorganisms, to achieve organic conversion of key equipment. It is widely used in food, beverage, medicine, cosmetics and other industries to provide suitable environment and conditions to promote the growth and metabolism of microorganisms, so as to achieve the transformation of organic matter. Function and effect Temperature control: Provides a stable temperature control system to ensure the stability of the temperature during the fermentation process. Humidity control: Some devices can control the relative humidity to provide a suitable growth environment for microorganisms. Gas environment: Provides a constant gas environment for the fermentation process, such as oxygen supply. Stirring system: Keep the fermentation liquid even and ensure better contact between the microorganisms and the substrate. Product characteristics Long duration of high temperature: it can continue to work above 65℃ for about 7 days, and above 55℃ for about 10 days to ensure adequate fermentation. Fermentation process emissions: strictly control the fermentation process, reduce harmful gas emissions, protect the environment and human health. Industry compliance: Meets the hygiene and safety standards of the food industry. Environmental protection and odorless: The use of molecular membrane technology to achieve waterproof, bactericidal, fluoroscopic and deodorizing functions to ensure environmental safety. Low operating costs: Fermentation of a ton of organic fertilizer only requires two hours of electricity, the cost is low. Intelligent features: After setting the program, the equipment can work automatically without manual intervention. Technical parameter Temperature range: +0°C to +55°C, some devices can reach +26°C. Humidity control: The relative
Product Attributes
| Brand | Yipomson |
|---|---|
| Min. Order | Piece/Pieces |
| Port | Yantian,Shekou,Nansha |
| Packaging | wooden |
| Supply Ability | 500PCS/month |
| Transportation | Ocean, Land, Express |
| Payment Type | T/T |
| Incoterm | FOB |
High quality factory price industrial high-tech bread baking machine price fermentation tank
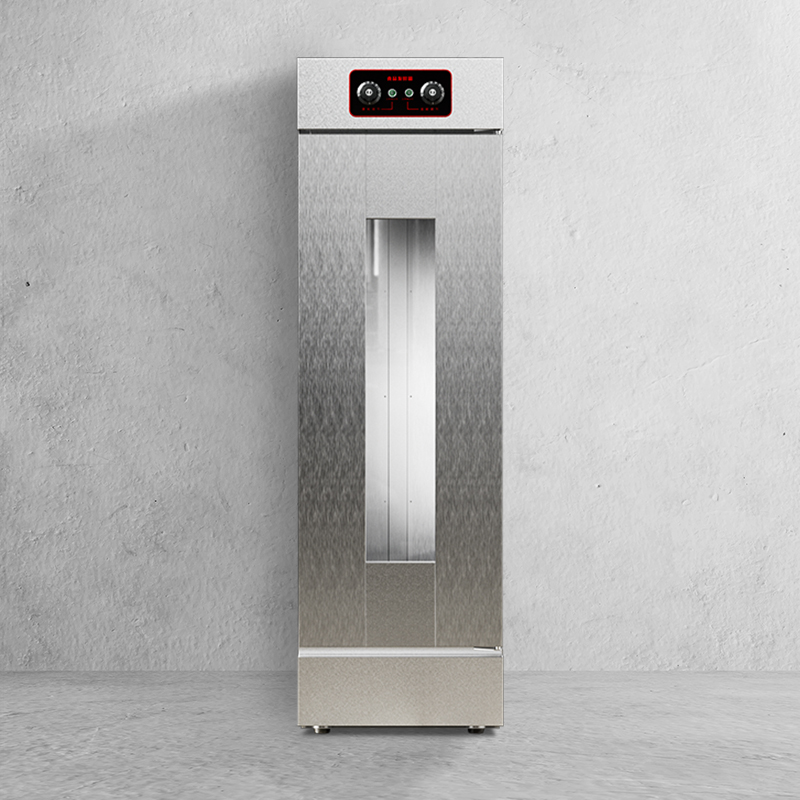
Product overview
Commercial food fermentation equipment is specially designed for the food industry, used to promote the growth
and metabolism of microorganisms, to achieve organic conversion of key equipment. It is widely used in food, beverage,
medicine, cosmetics and other industries to provide suitable environment and conditions to promote the growth and
metabolism of microorganisms, so as to achieve the transformation of organic matter.
Function and effect
Temperature control: Provides a stable temperature control system to ensure the stability of the temperature during
the fermentation process.
Humidity control: Some devices can control the relative humidity to provide a suitable growth environment for
microorganisms.
Gas environment: Provides a constant gas environment for the fermentation process, such as oxygen supply.
Stirring system: Keep the fermentation liquid even and ensure better contact between the microorganisms and
the substrate.
Product characteristics
Long duration of high temperature: it can continue to work above 65℃ for about 7 days, and above 55℃ for
about 10 days to ensure adequate fermentation.
Fermentation process emissions: strictly control the fermentation process, reduce harmful gas emissions,
protect the environment and human health.
Industry compliance: Meets the hygiene and safety standards of the food industry.
Environmental protection and odorless: The use of molecular membrane technology to achieve waterproof,
bactericidal, fluoroscopic and deodorizing functions to ensure environmental safety.
Low operating costs: Fermentation of a ton of organic fertilizer only requires two hours of electricity, the
cost is low.
Intelligent features: After setting the program, the equipment can work automatically without manual
intervention.
Technical parameter
Temperature range: +0°C to +55°C, some devices can reach +26°C.
Humidity control: The relative humidity control range is 40% to 95%.
Material: The structure is completely made of stainless steel 304, resistant to corrosion and high temperature.
Insulation material: polyurethane stainless steel insulation board.
Application scenario
Food industry: yogurt, fruit wine, beer and other fermented food production and research.
Pharmaceutical industry: production of antibiotics, vaccines and other biological products.
Chemical engineering: fermentation to produce organic acids, amino acids and other chemicals.
Biological research: Provide experimental platform for microbiology and biochemistry research.
————————————
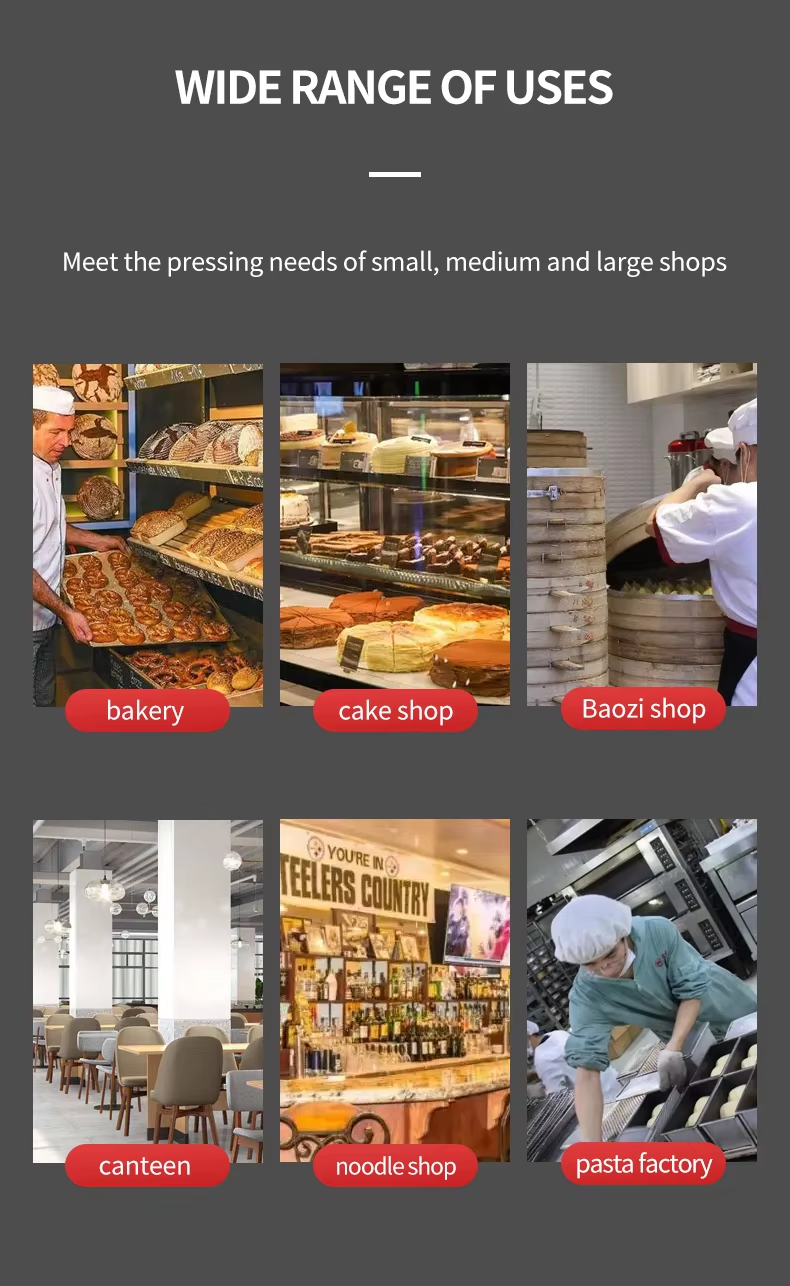
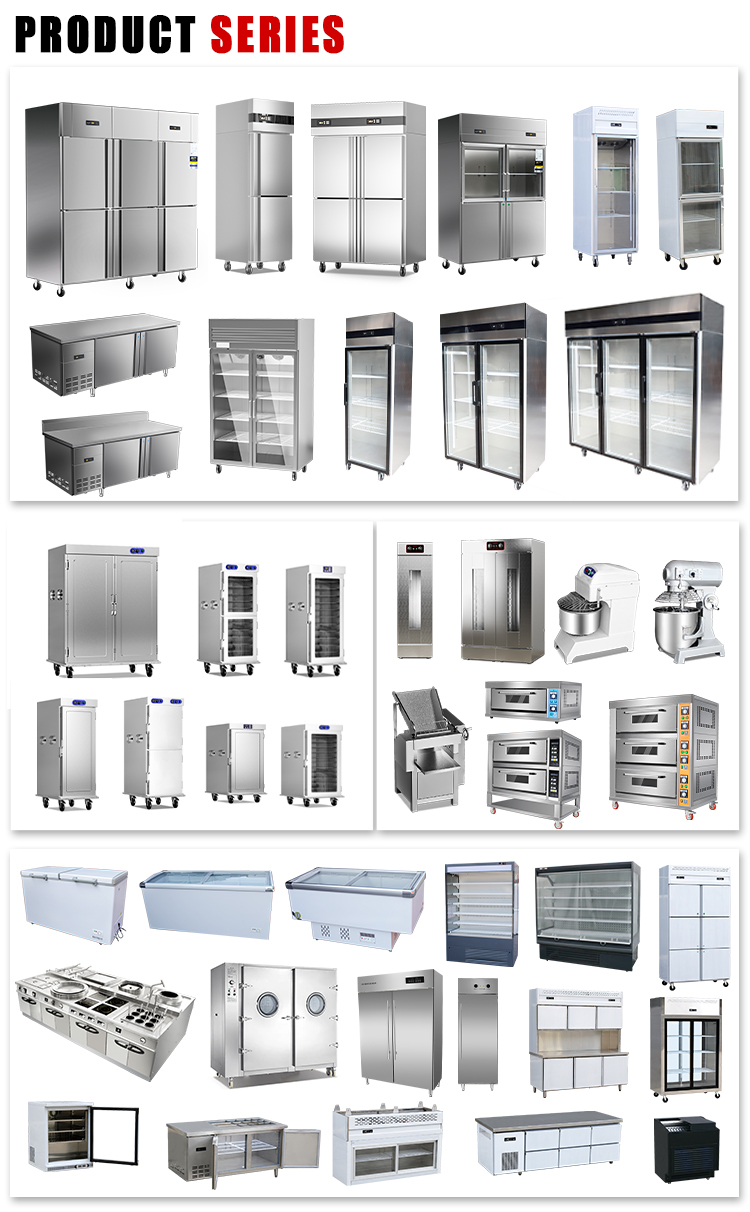
We are a professional manufacturer of commercial refrigerator and have extensive experience
in the manufacturing of bakery equipment ,We also produce western kitchen Equipment.
Our wide range of products includes commercial refrigerators with excellent refrigeration
and steamed rice cabinet for different scenarios.
In addition, we also provide high temperature intelligent disinfection cabinet with intelligent
control of high temperature and launch restaurant warmer dining cart with excellent thermal
insulation performance.
In the bakery industry, our equipment is trusted by customers, such as high capacity
commercial oven for bakery, and advanced spiral dough mixer.We also provide stable
electric dough fermenting proofer to meet the stringent requirements of different customers
for the baking process.
If you are interested in our products, or have any customization needs, please contact us.
We sincerely look forward to establishing long-term cooperative relations with you and jointly
expand the market!
Volume pricing
| Minimum quantity | Unit | Unit price |
|---|---|---|
| 1 | Piece/Pieces | USD 155.0000 |
| 50 | Piece/Pieces | USD 135.0000 |
Product Videos
You May Also Like
-
 Commercial dough proofing machine
Commercial Electric Pizza Proofer Fermenting Machine Bakery Equipmenrt Fermenter Dough Bakery Kitchen Proofer [Product name] : Commercial pastry fermentation machine [Product specification] : 1000mm x 640mm x 1620mm [Product weight] : 250kg [Product material] : Stainless steel 304, corrosion resistance, easy to clean [Product capacity] : It can accommodate 26 standard pastry trays at the same time, each tray size is 600mm x 400mm [Temperature control] : 0℃~40℃, accurate temperature control, to ensure the fermentation effect [Humidity control] : 70%~95%, automatic humidification, keep the dough moist 【 Product function 】 : 1. Dough fermentation: suitable for all kinds of Chinese and Western pastry fermentation, such as steamed bread, bread, pizza, etc. 2. Constant temperature and humidity: automatically adjust the internal environment to ensure the best conditions during dough fermentation. 3. Timing switch: Users can set the fermentation time according to their needs, and automatically stop working after fermentation is completed. 4. Audible and visual alarm: When the temperature or humidity exceeds the preset range, the device will issue an audible and visual alarm. 【 Product Features 】 : 1. Automatic control, easy operation, no need to guard. 2. Stainless steel, durable, easy to clean. 3. Large capacity design, suitable for mass production. 4. Precise temperature and humidity control ensures the consistency of fermentation effect. 5. Energy saving and environmental protection, low operating cost. [Application Scenario] : 1. Commercial bakery 2. Hotel canteen 3. School cafeteria 4. Bread baking factory 5. Restaurant chains 【 After-sales service 】 : We provide one year warranty service, lifetime maintenance. If you encounter any problems during use, you can contact us at any time, and we will solve it for you as soon as possible. The above is the product details page of our commercial pastry fermentation machines, please feel free to contact us if you have any quest
-
 Commercial Proofing Single/Double Door & Combo Cabinet
Yipomson Commercial Proofing Box – Single/Double Door & Combo Proofing & Baking Cabinet Product Overview The Yipomson Commercial Proofer is designed for bakeries, pizzerias, and commercial kitchens to ensure perfect dough fermentation every time. Available in single-door, double-door, and comboer proofing & baking models, these cabinets provide precise temperature and humidity control for consistent, high-quality results. Key Features & Benefits ✔ Precise Fermentation Control – Adjustable temperature (68°F–122°F / 20°C–50°C) and humidity (50%–90%) for optimal dough rising. ✔ Multiple Models Available – Choose from single-door, double-door, or combo proofing & baking units for different kitchen needs. ✔ Stainless Steel Construction – Durable, rust-resistant, and easy to clean. ✔ Uniform Heating & Humidity – Advanced airflow system ensures even fermentation. ✔ Energy Efficient – Insulated walls retain heat, reducing power consumption. ✔ Easy-to-Use Digital Panel – Intuitive controls for hassle-free operation. ✔ Safety Features – Overheat protection and auto shut-off for safe use. Available Models 1. Single-Door Proofing Capacity: OEM Power: 110V / 1500W 2. Double-Door Proofing Capacity: OEM Power: 220V / 3000W 3. Combo Proofing & Baking Oven Proofing & Baking in One Unit – Switch between modes for efficiency. Capacity: OEM Power: 220V / 3500W Technical Specifications Brand: Yipomson Material: 304 Stainless Steel Temperature Range: 68°F–122°F (20°C–50°C) Humidity Range: 50%–90% Warranty: 1-Year Limited Warranty Why Choose Yipomson? ✅ Professional-Grade Quality – Trusted by bakeries and restaurants worldwide. ✅ Versatile Options – Single-door, double-door, and combo models available. ✅ Energy-Saving Design – Reduces operational costs. ✅ Easy Maintenance – Smooth surfaces for quick cleaning. Ideal For: Bakeries & Patisseries Pizzerias & Bread Shops Hotels & Catering Services Commercial Kitchens ———————————— We are a professional manufacturer of commercial refrigerator an
-
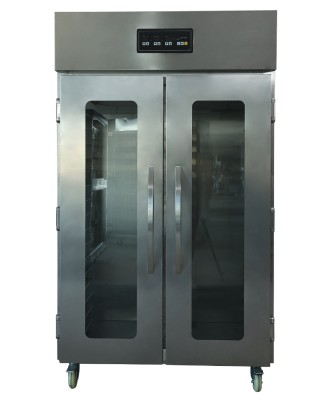 32-Tray Electric Bakery Fermentation Cabinet
Stainless Steel Automatic Dough Proofing Cabinet for Bread Bakery with Humidity & Temperature Control System Product Overview The Yipomson 32-Tray Commercial Double Door Dough Proofer is the perfect choice for large bakeries and food production facilities. With its intelligent digital control system and generous capacity, it ensures stable temperature and humidity for uniform dough fermentation. The twin glass doors offer clear visibility inside while maintaining insulation, making your workflow more efficient and professional. This high-performance machine supports even proofing , easy mobility , and custom branding , all built into a durable stainless steel body . Key Features 32-Tray Large Capacity Designed to hold 32 baking trays (600×400 mm standard) to meet large-scale fermentation needs. Digital Touch Control Panel Set temperature, humidity, and timer with precision using a user-friendly interface. Adjustable Proofing Conditions Temperature range from 30–40°C and humidity range from 60–95% RH, perfect for all types of dough. Double-Layer Tempered Glass Doors Retains heat and moisture while allowing users to monitor dough progress. Heavy-Duty Stainless Steel Construction Hygienic, easy to clean, and built for long-term commercial use. Built-in Humidification System Provides consistent steam to support soft, fluffy bread and pastry textures. Smooth Caster Wheels with Locks Easy to move and fix in place, ideal for flexible kitchen layout adjustments. OEM/ODM Available Voltage, tray size, branding logo, and control panel can be customized for different markets. Technical Specifications Parameter Specification Brand Yipomson Model YP-PF32 Type Double Door Commercial Dough Proofer Retarder Capacity 32 Trays (600×400 mm or customized) Material SUS304 Stainless Steel Temperature Range 30°C – 40°C (86°F – 104°F) Humidity Range 60% – 95% RH (adjustable) Control Panel Digital touch display Doors Double glass doors (tempered and insulated) Humidification Internal steam s
-
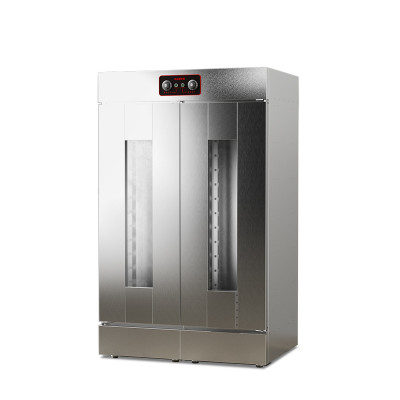 26 Trays Double Door Proofer Fermenting Machine
Commercial Use OEM Custom Ce Approved 26 Trays Double Door Professional Dough Proofer Fermenting Machine For Bread Making Designed specifically for bakeries and commercial baking environments for the fermentation process of dough, the commercial Bread Electric Durable fermentation equipment is a key tool to improve the quality and efficiency of bread production, they help bakers make better bread products by precisely controlling the fermentation conditions. One key operation Temperature and humidity double control fermentation to wake up delicate taste. High strength sheet metal High-strength sheet metal, long life, corrosion resistance. Pure copper tube evaporator Using pure copper tube evaporator, the evaporation is faster and the efficiency is higher. GB Power Cord Safety and Durability. ———————————— We are a professional manufacturer of commercial refrigerator and have extensive experience in the manufacturing of bakery equipment ,We also produce western kitchen Equipment. Our wide range of products includes commercial refrigerators with excellent refrigeration and steamed rice cabinet for different scenarios. In addition, we also provide high temperature intelligent disinfection cabinet with intelligent control of high temperature and launch restaurant warmer dining cart with excellent thermal insulation performance. In the bakery industry, our equipment is trusted by customers, such as high capacity commercial oven for bakery, and advanced spiral dough mixer.We also provide stable electric dough fermenting proofer to meet the stringent requirements of different customers for the baking process. If you are interested in our products, or have any customization needs, please contact us. We sincerely look forward to establishing long-term cooperative relations with you and jointly expand the market!
-
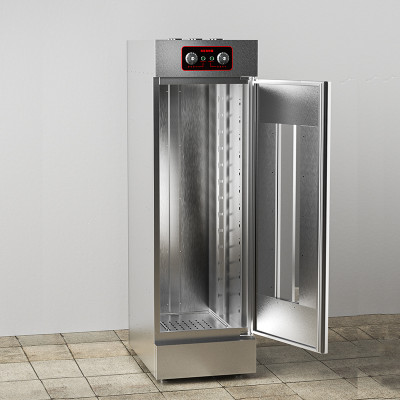 Fermentation box for pizza dough
Commercial Multifunctional Automatic Stainless Steel Electric Dough Retarder Proofer Fermentation New Bakery Restaurant Use Commercial single door fermentation box is a kind of professional equipment used for food processing, especially in the fermentation process of bread, cake and other baked goods. It provides an ideal fermentation environment for food by controlling temperature and humidity to ensure the quality and taste of the product. The following is a detailed introduction to the commercial single-door fermentation tank: 1. Temperature control: The fermentation tank can accurately adjust the internal temperature, usually between room temperature and 45 ° C, different models of products may have different temperature adjustment ranges. This is essential for different fermentation needs (e.g. yeast fermentation, enzyme activity maintenance, etc.). 2. Humidity control: In addition to temperature, humidity is also an important factor affecting the fermentation process. Most commercial fermentation tanks are equipped with a humidification function, which can maintain a certain humidity level in the box, helping to prevent the dough surface from drying and forming a hard shell, ensuring the fermentation effect. 3. Timing function: Many fermentation tanks are also equipped with the function of timing off, the user can set the fermentation time according to the need, the equipment will automatically stop working after reaching the set time, convenient and practical. 4. Material and design: Commercial fermentation tanks are usually made of stainless steel or food-grade plastic, easy to clean and durable. It is designed with ease of use and safety in mind, such as transparent glass doors for easy viewing of the inside, and anti-hot handles for safe handling. 5. Capacity size: According to different business needs, fermentation tanks have a variety of capacity specifications, from small suitable for home or small bakery use, to large enterprise products suitable for m
-
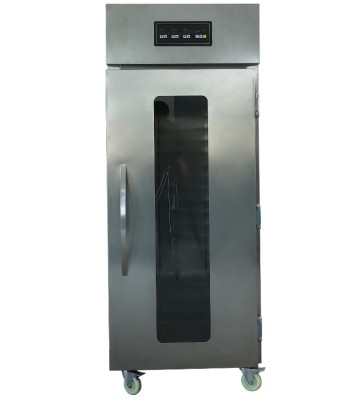 Fermentation Cabinet for Dough Proofing and Retarding
Stainless Steel Automatic Bread Dough Proofer for Bakery Kitchen with Humidity & Temperature Control System The Yipomson 16-Tray Commercial Electric Dough Proofer is specially designed for professional bakeries, pastry kitchens, restaurants, and food processing plants. With precise temperature and humidity control, it provides the ideal environment for yeast activation and dough fermentation. The unit ensures consistent proofing results for bread, buns, croissants, and other bakery items. This proofer features a durable stainless steel exterior , a large viewing window , and a touch-sensitive digital control panel , making it efficient, hygienic, and easy to operate. Key Features 16-Tray Capacity Holds 16 bakery trays (standard 600×400 mm) to handle high-volume proofing needs. Intelligent Digital Control Panel Easy-to-use interface to set and monitor temperature, humidity, and proofing time. Temperature & Humidity Control Adjustable temperature (30–40°C) and humidity (60–95%) for optimal fermentation conditions. Stainless Steel Construction Strong, easy to clean, and suitable for long-term food-grade use. Double-Layer Insulated Door with Viewing Window Keeps internal heat and humidity stable while letting you monitor progress. Built-in Humidification System Maintains consistent moisture levels, essential for soft, fluffy baked goods. Caster Wheels with Brake Easy mobility for cleaning and layout adjustment; two wheels lock for stability. OEM & ODM Support Logo printing, voltage customization, tray size, and packaging available upon request. Technical Specifications Parameter Specification Brand Yipomson Model YP-PF16 Type Commercial Electric Dough Proofer Retarder Capacity 16 Trays (600×400 mm or customized) Material SUS304 Stainless Steel Temperature Range 30°C – 40°C (86°F – 104°F) Humidity Range 60% – 95% RH (adjustable) Control Panel Digital touch control Viewing Window Yes – clear tempered glass Humidification Built-in steam generator Power Supply 220V/50Hz (cu
-
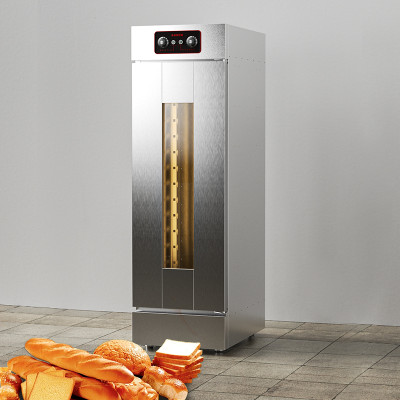 Full Stainless Steel Electric Fermenting Proofer Machine
Commercial 13Trays With Timer Hotel Restaurant Commercial Bread Electric Durable Fermenting Equipment Bakery Dough Proofer Designed specifically for bakeries and commercial baking environments for the fermentation process of dough, the commercial Bread Electric Durable fermentation equipment is a key tool to improve the quality and efficiency of bread production, they help bakers make better bread products by precisely controlling the fermentation conditions. One key operation Temperature and humidity double control fermentation to wake up delicate taste. High strength sheet metal High-strength sheet metal, long life, corrosion resistance. Pure copper tube evaporator Using pure copper tube evaporator, the evaporation is faster and the efficiency is higher. GB Power Cord Safety and Durability. —————————— We are a professional manufacturer of commercial refrigerator and have extensive experience in the manufacturing of bakery equipment ,We also produce western kitchen Equipment. Our wide range of products includes commercial refrigerators with excellent refrigeration and steamed rice cabinet for different scenarios. In addition, we also provide high temperature intelligent disinfection cabinet with intelligent control of high temperature and launch restaurant warmer dining cart with excellent thermal insulation performance.